Portable Line Boring & Pin Bore Repair for Heavy Equipment Across Nevada
DBM’s field service trucks carry portable line boring and bore welding systems directly to your jobsite, where technicians build up worn, oval pin bores with weld and machine them back to round, in-line OEM dimensions without dismantling the machine or hauling its frame to a machine shop.
Staged routes providing immediate highway and off-road transit coverage along the I-80 corridor, the Carlin Trend mining districts, US-95, and US-93.
Is Line Boring the Repair This Machine Needs?
Line boring is the repair when pin bores have worn out of round, which shows up as slop in an excavator boom or stick, a loader bucket that clunks and shifts before the hydraulics take the load, articulation joints that knock on a loader or haul truck, or new pins and bushings that work loose within weeks because the bore around them is no longer round.
New pins and bushings fitted into an oval bore wear out quickly, so the technician measures every bore at the joint before quoting and confirms whether the joint needs line boring, bore welding, or only new pins and bushings.
If you cannot tell which joint is worn, call (775) 625-0062 and describe what the machine does under load, and the technician who inspects the machine locates the worn bore before any work is priced.
Machines, Pin Joints & Bore Sizes We Line Bore
Equipment
- Excavators and mining shovels
- Wheel loaders
- Dozers
- Articulated and rigid haul trucks
- Cranes
- Other heavy equipment from any manufacturer, including machines DBM did not sell
Pin Joints & Bores
- Boom, stick, and bucket pivots on excavators and shovels
- Lift arm, bucket, and linkage pins on wheel loaders
- Articulation joints and center hinges
- Equalizer bars and track frame mounts
- Hydraulic cylinder eyes and clevis mounts
- Bucket ears and attachment mounting lugs
On-Site Line Boring & Shop Machining
Portable Line Boring at the Jobsite
Portable boring bars mount directly on the machine where it stands at the jobsite, quarry, or mine, so the frame stays assembled and in place and you avoid heavy-haul freight, permits, and the labor of removing major components.
- DISPATCH
- Field crews usually reach the machine the day after you call and sometimes the same day, while the machine makers’ dealers often take one to three weeks to get a technician to a job.
- DOWNTIME
- A single joint bored, welded, and fitted with new pins and bushings in the field typically takes one to two days once parts are on site, and the technician confirms the time after measuring the bores.
- SERVICE TRUCKS
- Each service truck carries its own generator, crane, and tooling, so the job needs no power or lifting equipment from your site.
- SERVICE AREA
- All of Nevada, including remote mine sites along the I-80 corridor and the Carlin Trend.
Shop Line Boring for Major Overhauls
Components that need a full rebuild, and castings too badly cracked or worn to repair in place, are removed and machined in our shop, where the part is set up, supported, and aligned for heavier weld build-up and boring.
- WHEN
- Major overhauls, damaged castings, and components such as buckets, booms, and sticks that are already off the machine.
- PICKUP
- You can deliver components to the shop, or our crane trucks collect them from the jobsite.
- DOWNTIME
- Shop jobs are scheduled after inspection, and the quote states the completion date.
Bore Welding, Pins & Bushings, and Crack Repair
Bore Welding & Re-Boring to OEM Size
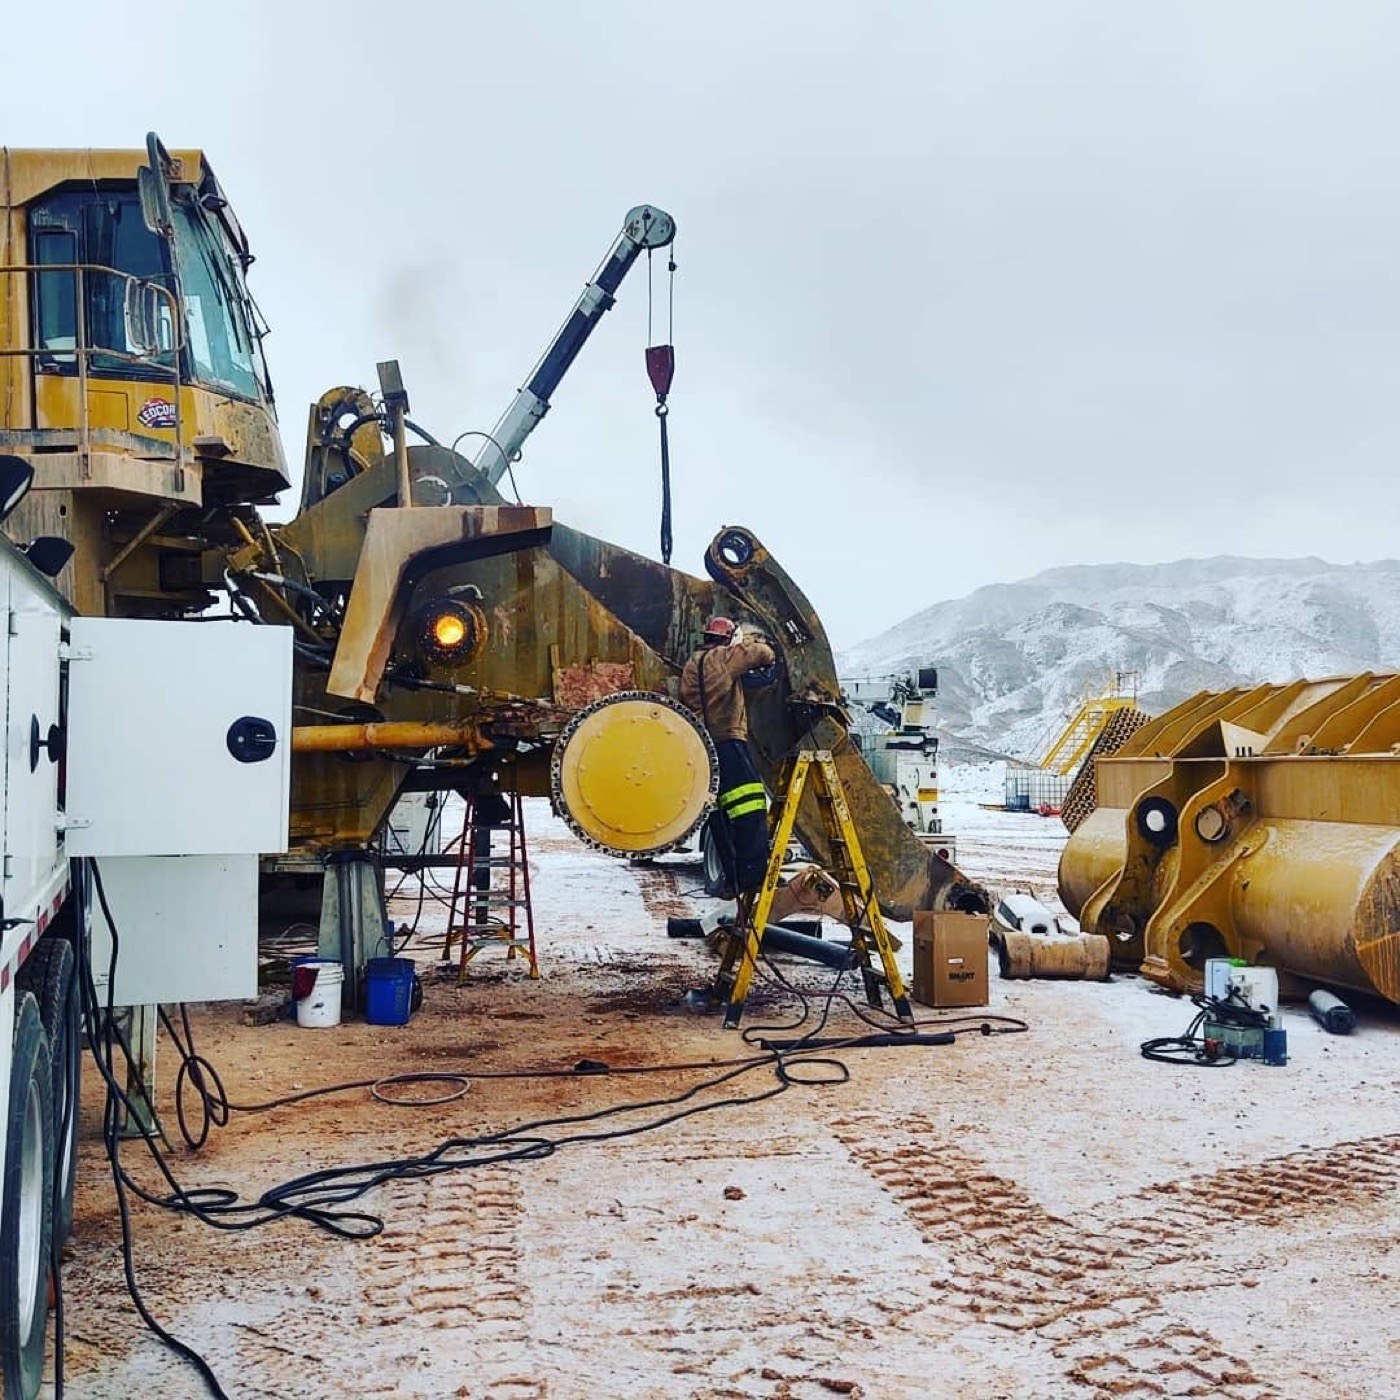
An oval bore cannot be machined round without removing more metal, so worn bores are built back up with weld before they are bored to size.
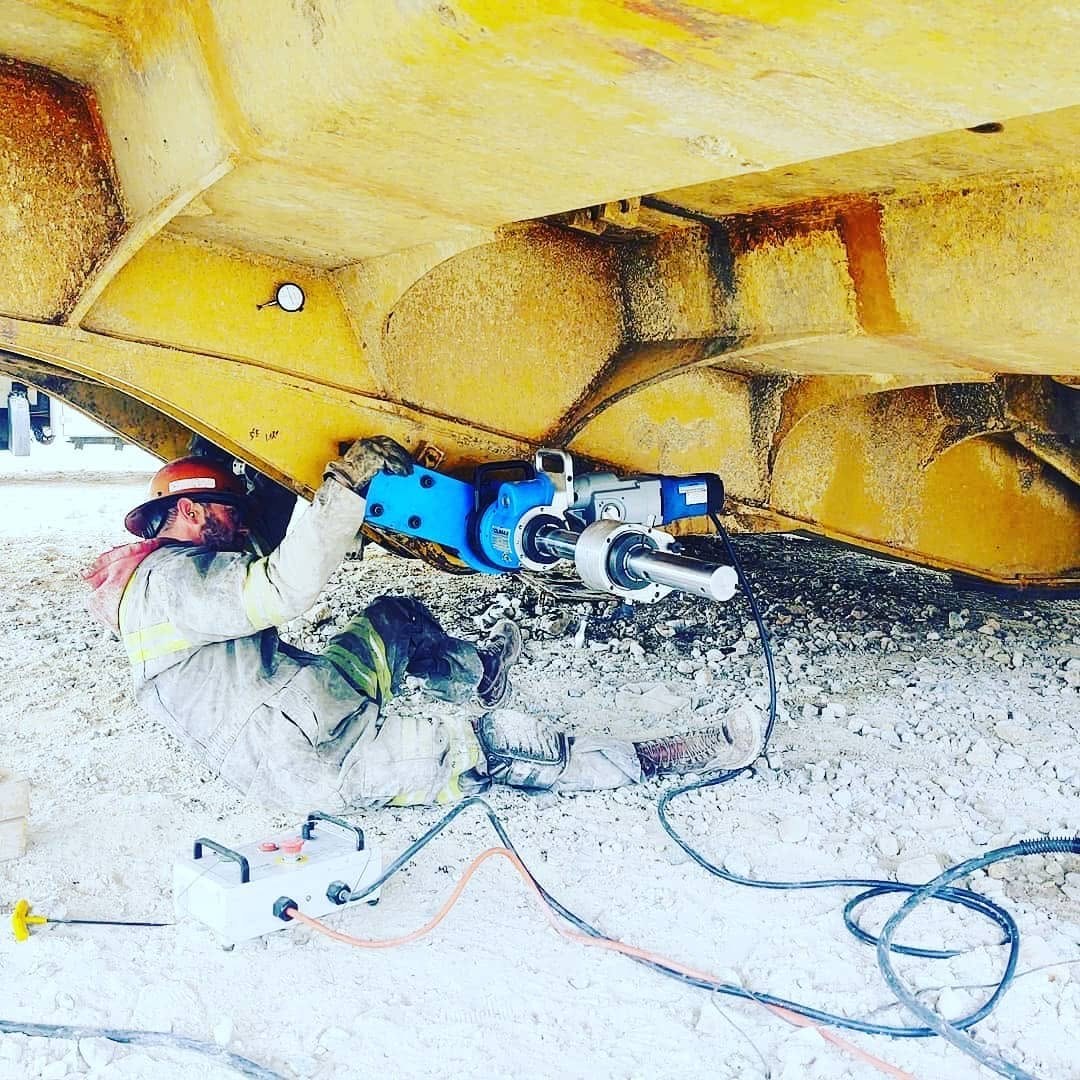
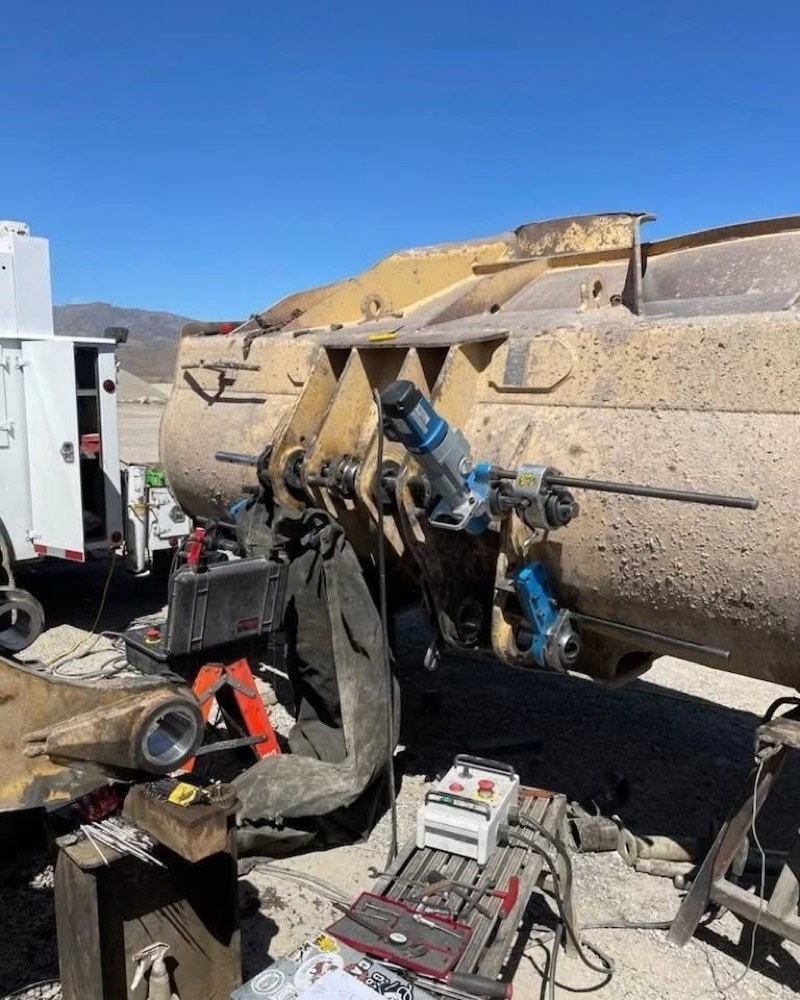
- The technician sets the portable boring bar through the joint and bores out the worn, out-of-round surface to clean metal.
- An automated bore welder lays weld around the inside of each bore to add fresh structural material.
- The boring bar machines each welded bore back to round at the original OEM diameter, within ±.001 inch and in line with the matching bore on the other side of the joint.
Pin & Bushing Replacement
New pins and bushings go into the finished bores as part of the same job, so the joint leaves the repair complete.
- Old bushings are pressed or cut out before the bores are machined.
- New bushings are installed by freeze-fitting them in liquid nitrogen or by pressing them in, depending on their size and fit.
- Our parts department supplies pins and bushings for XCMG and SAS machines and sources aftermarket pins and bushings for most other equipment, and we machine custom pins when no standard part fits.
Crack Inspection & Structural Repair Around the Bore
The bosses and lugs that carry a worn pin often crack, so the steel around each bore is inspected before machining begins.
- The technician checks the bosses and lugs around each bore with magnetic particle inspection, a non-destructive test that shows surface cracks the eye cannot see.
- Cracks are gouged out and repaired with structural welding by AWS-qualified welders before the bore is welded and machined.
- Cracks in booms, frames, or other structural steel away from the bore are repaired by the same field crew as part of our welding and fabrication service.
Line Boring Equipment & Technician Qualifications
- Climax · Portable
Portable Line Boring & Bore Welding Systems
Field and shop line boring runs on Climax portable boring bars and automated bore welders, which machine bores from 1.5 to 12 inches in diameter to within ±.001 inch of the original OEM size.
- Laser Aligned
Bore Alignment Before Machining
The bores on both sides of a joint are aligned with each other by laser or optical alignment before boring begins, so the new pin seats straight and the bushings wear evenly.
- AWS D1.1 · D1.14
AWS Certified Welding
Every bore weld and structural repair is executed by technicians holding active qualifications under AWSAmerican Welding Society, which publishes the structural welding codes. D1.1 (Structural Steel Code) and AWS D1.14 (Earthmoving, Construction, and Agricultural Equipment Code).
- MSHA Part 46 · Part 48
Mine Site Readiness
Field technicians maintain active Mine Safety and Health Administration (MSHA) Part 46 and Part 48 certifications for surface mining operations and arrive with the mandated PPEPersonal protective equipment. to pass mine gates without administrative delay.
Line Boring Field Work
- Pivot Joint
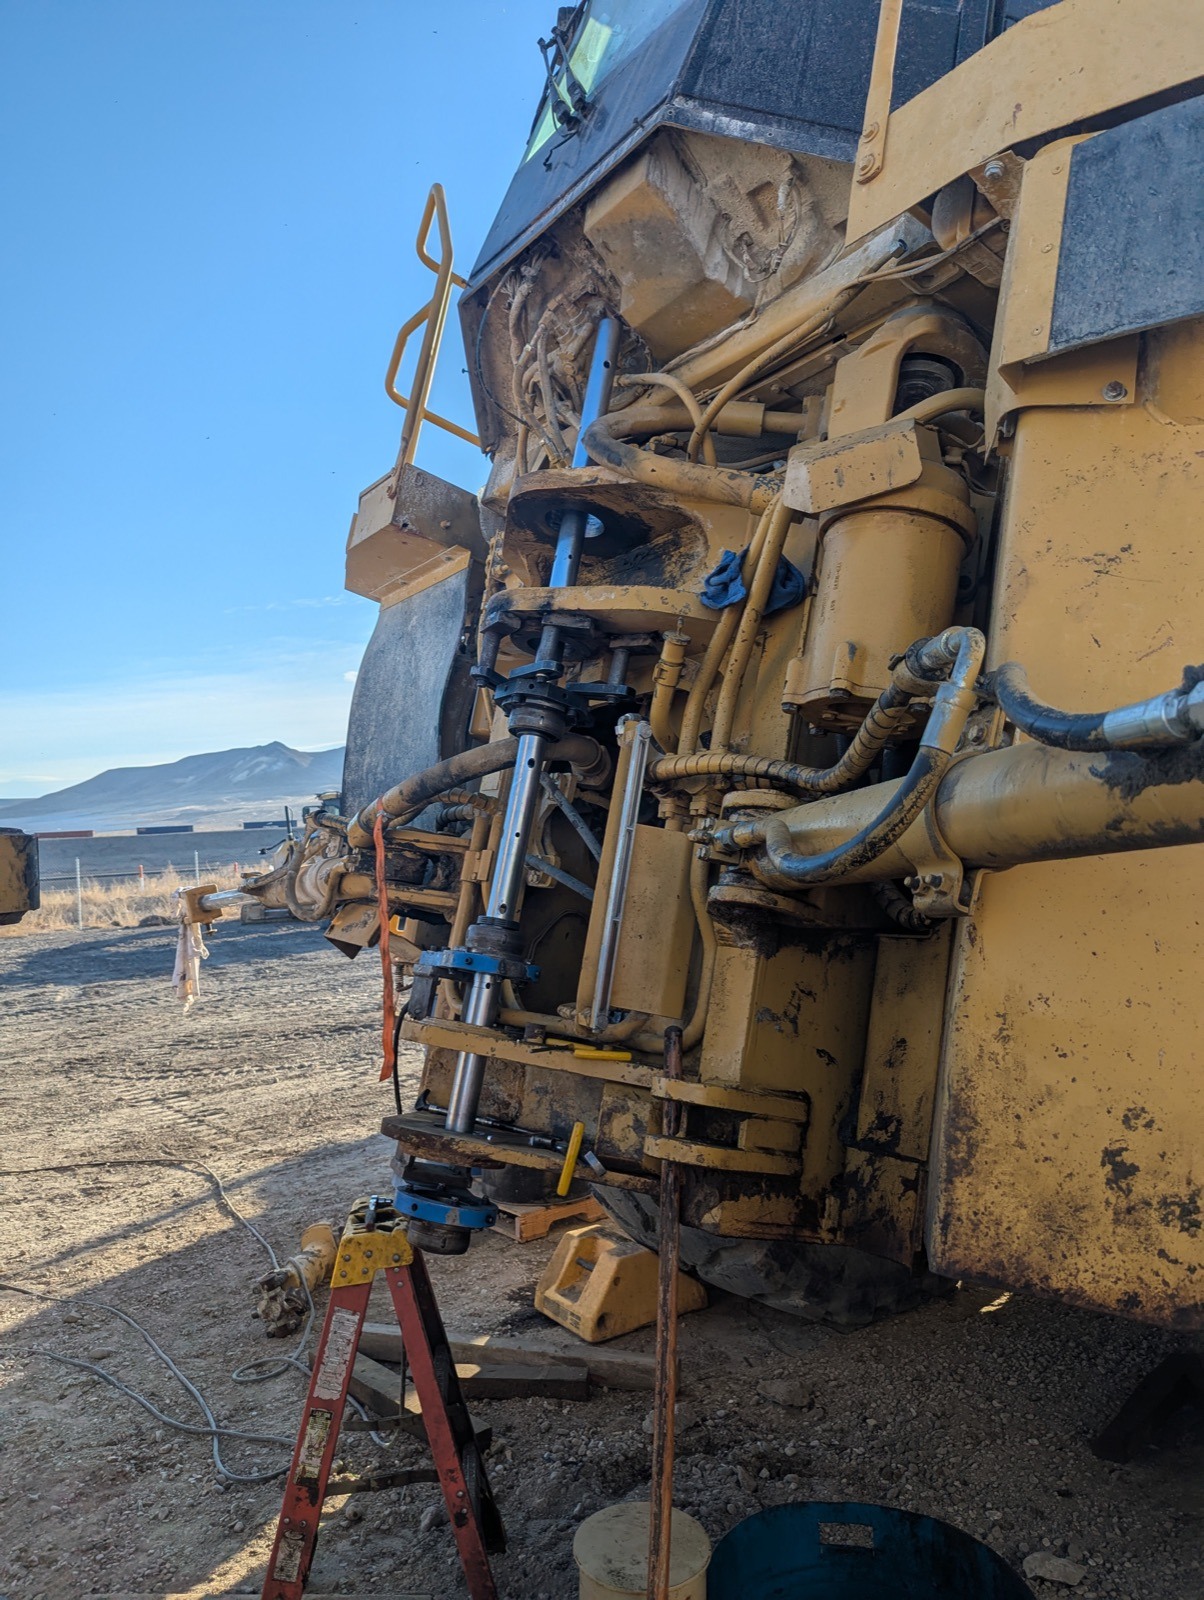
Portable boring machine set on the pivot joint of a large wheeled machine, with the machine left in place at the jobsite and stepladders giving access to the bore.
- Truck-Mounted Boring
Machine arm supported in a lifting sling while a portable boring machine mounted on the service truck’s rear deck machines the bore at its end.
- Cylinder Eye
Portable line boring machine clamped to the end of a large cylinder, powered from the generator in the service truck’s tool body.
- Mine Site
DBM service trucks staged at a large mining excavator, carrying the tooling and power for field repairs at a remote mine.
Line Boring Quotes & Job Sequence
How Line Boring Jobs Are Quoted
Line boring is quoted per job after a technician measures the worn bores, because the price depends on how many bores the joint has, their diameter, and how much weld build-up each one needs.
- INSPECTION
- The technician measures each bore for wear and ovality at the jobsite or in our shop before a price is given.
- QUOTE
- The quote itemizes labor hours, weld build-up, pins, bushings, and any crack repair, and no work order is authorized until you approve it.
- TRAVEL
- Field jobs bill travel time portal-to-portal, from our Fernley yard gate to the machine’s location and back.
- CALL-OUT
- A flat-rate call-out minimum covers mobilization and the initial bore inspection.
- PARTS
- We call you with the parts cost and lead time, including the option to pay for overnight shipping, and order nothing until you choose.
How a Line Boring Job Runs
STEP 1 OF 4Line Boring Request & Photo Upload
Line Boring Questions
We line bore excavators, mining shovels, wheel loaders, dozers, haul trucks, cranes, and other heavy equipment from any manufacturer, including machines DBM did not sell.
Field crews usually arrive the day after you call. A single joint bored, welded, and fitted with new pins and bushings in the field typically takes one to two days once parts are on site, and the technician confirms the time after measuring the bores. Overnight shipping is available when the pins or bushings are not in stock.
A photo helps us plan the job, but the price depends on how far the wear goes, so we price the work after a technician has measured the bores.
Use the request form on this page, which takes a close view of the worn bore or pin and a wide view of the joint straight from your phone’s camera and sends them to the service manager with the machine details.
Yes. When a repair will keep your machine down for an extended shop job, we coordinate with our rental fleet to put a matching machine on your jobsite so the work keeps running.
Yes. Our parts department supplies pins and bushings for XCMG and SAS machines and sources aftermarket pins and bushings for most other equipment, so the parts for the job come from DBM.
Other DBM Services
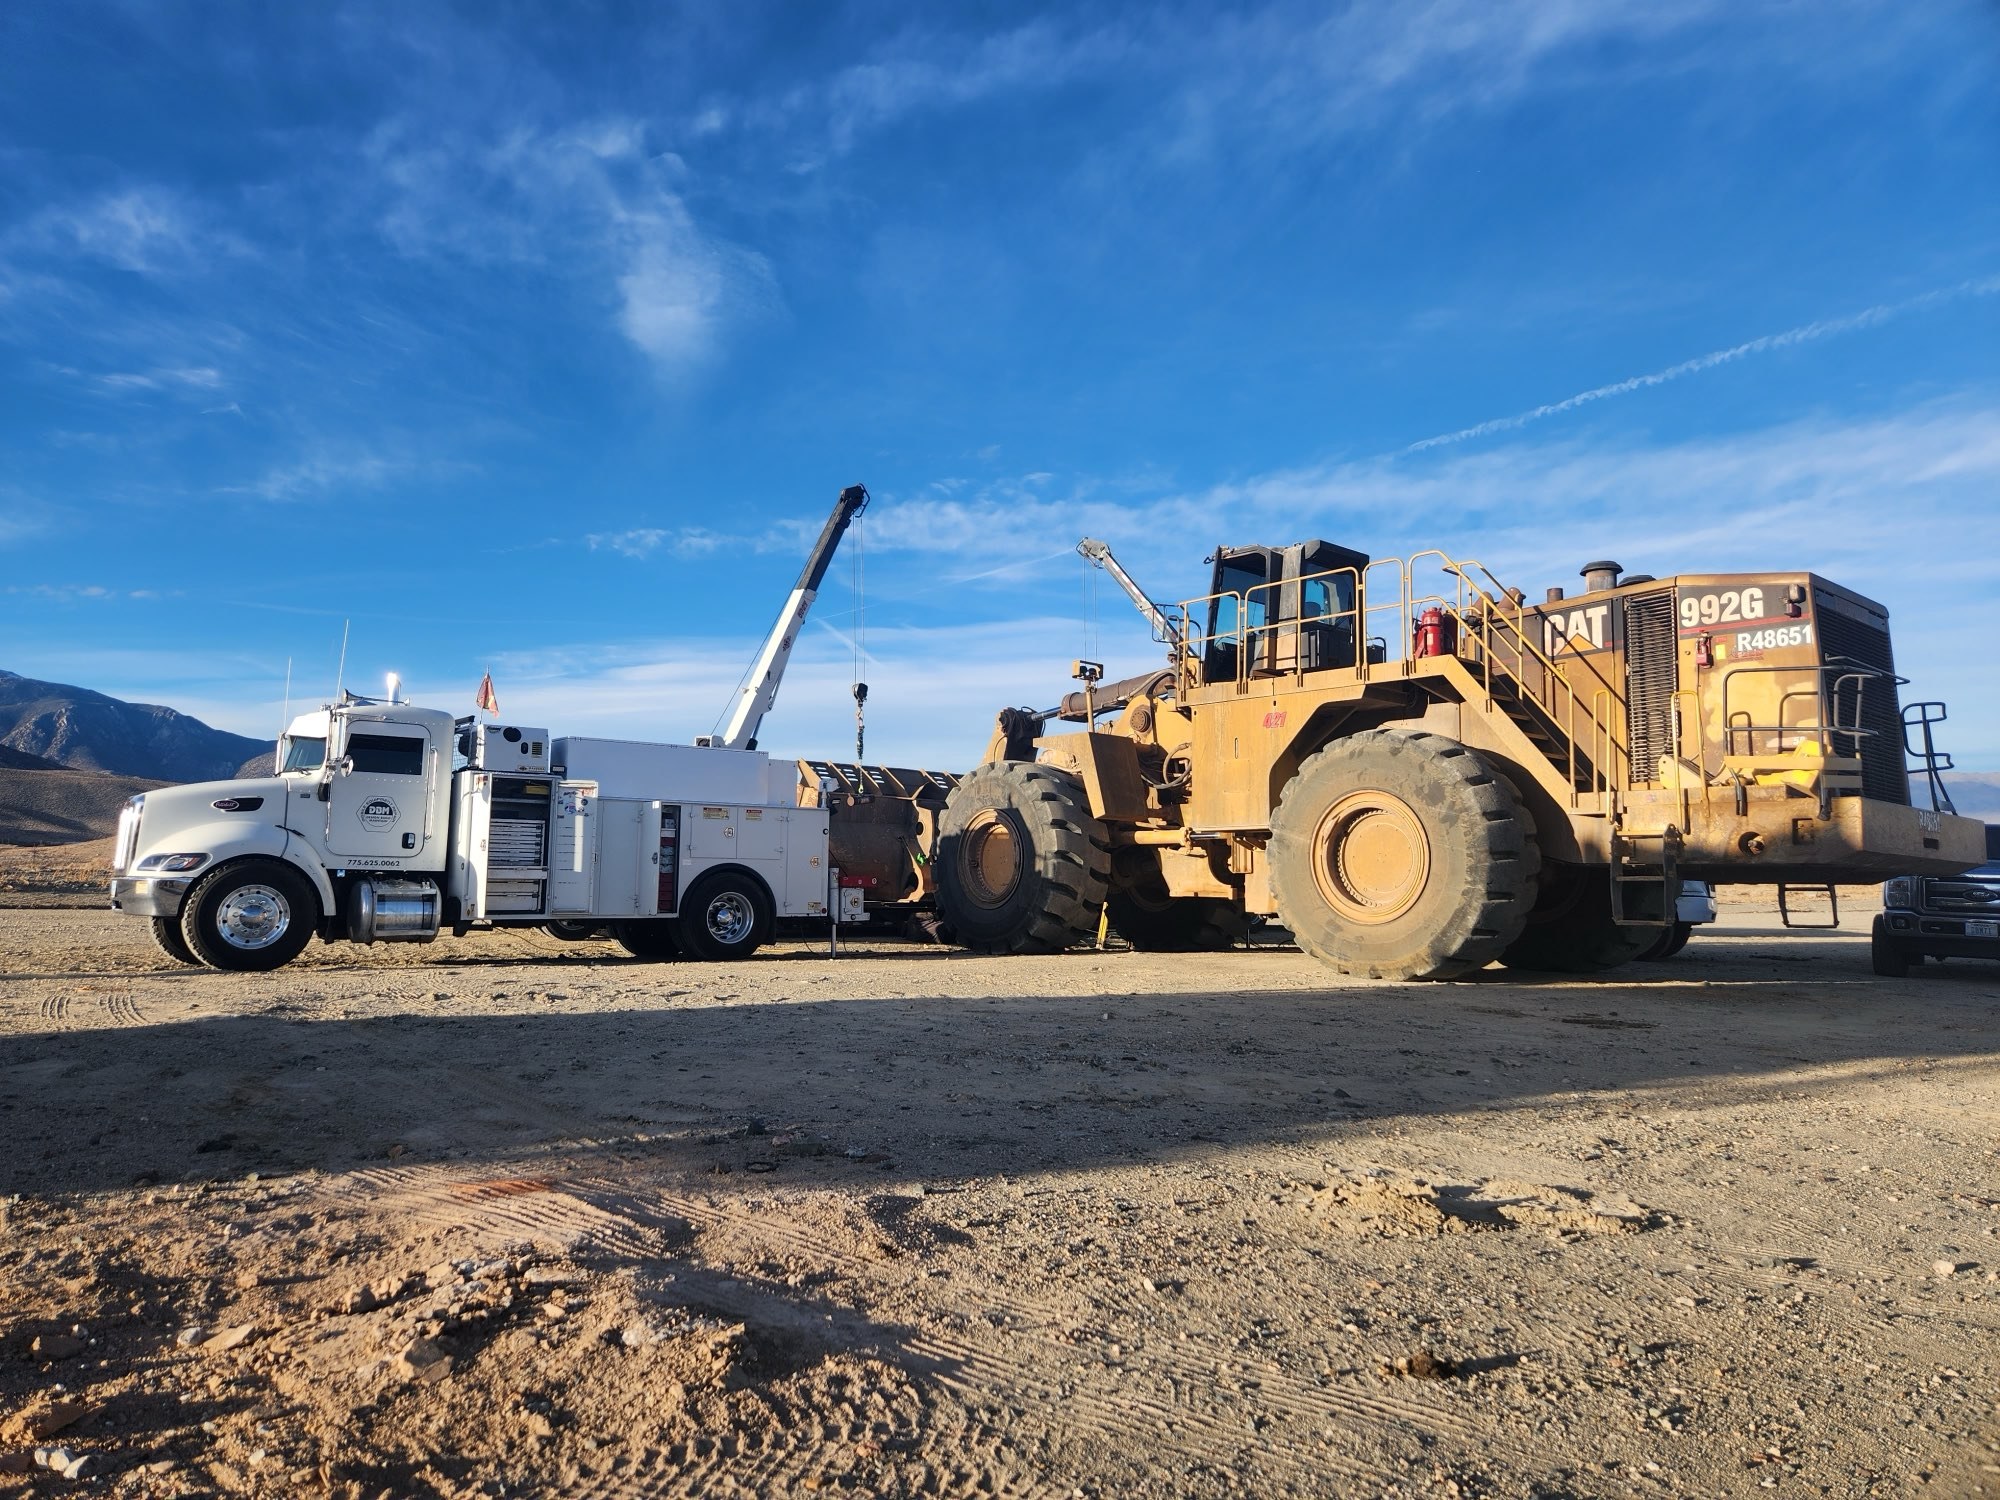 Mobile field serviceOur service trucks carry the tools and power to repair machines at mines and construction sites across Nevada, so the machine is fixed where it is working.
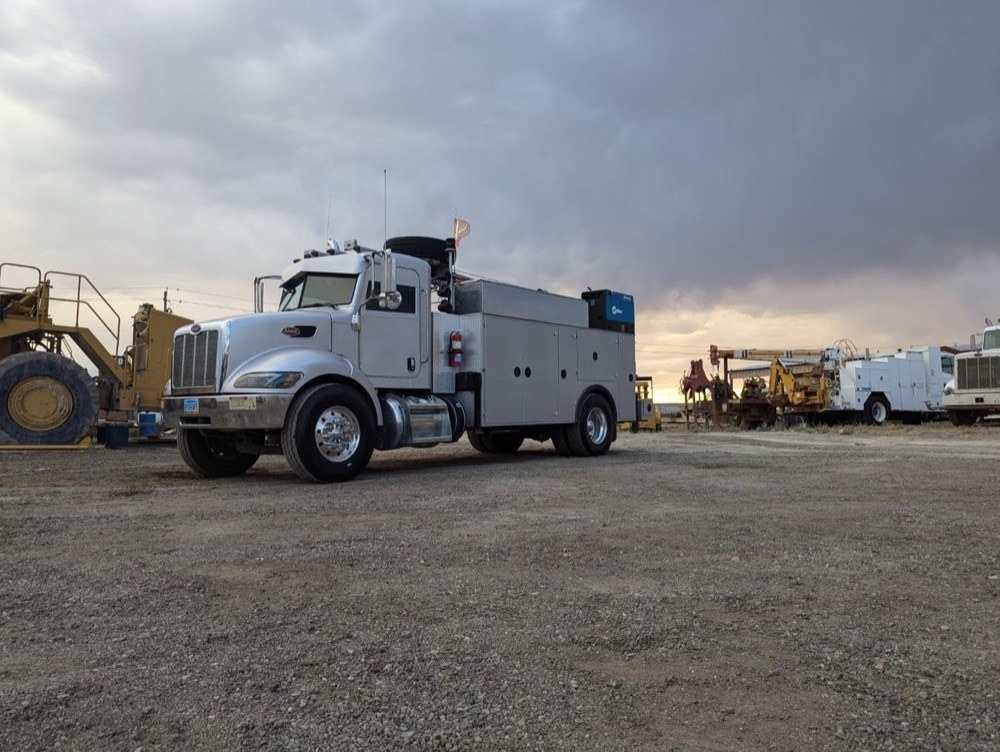 Welding and fabricationMobile structural welding, gouging, and hardfacing for cracked and worn heavy equipment steel, at the jobsite or in our shop.
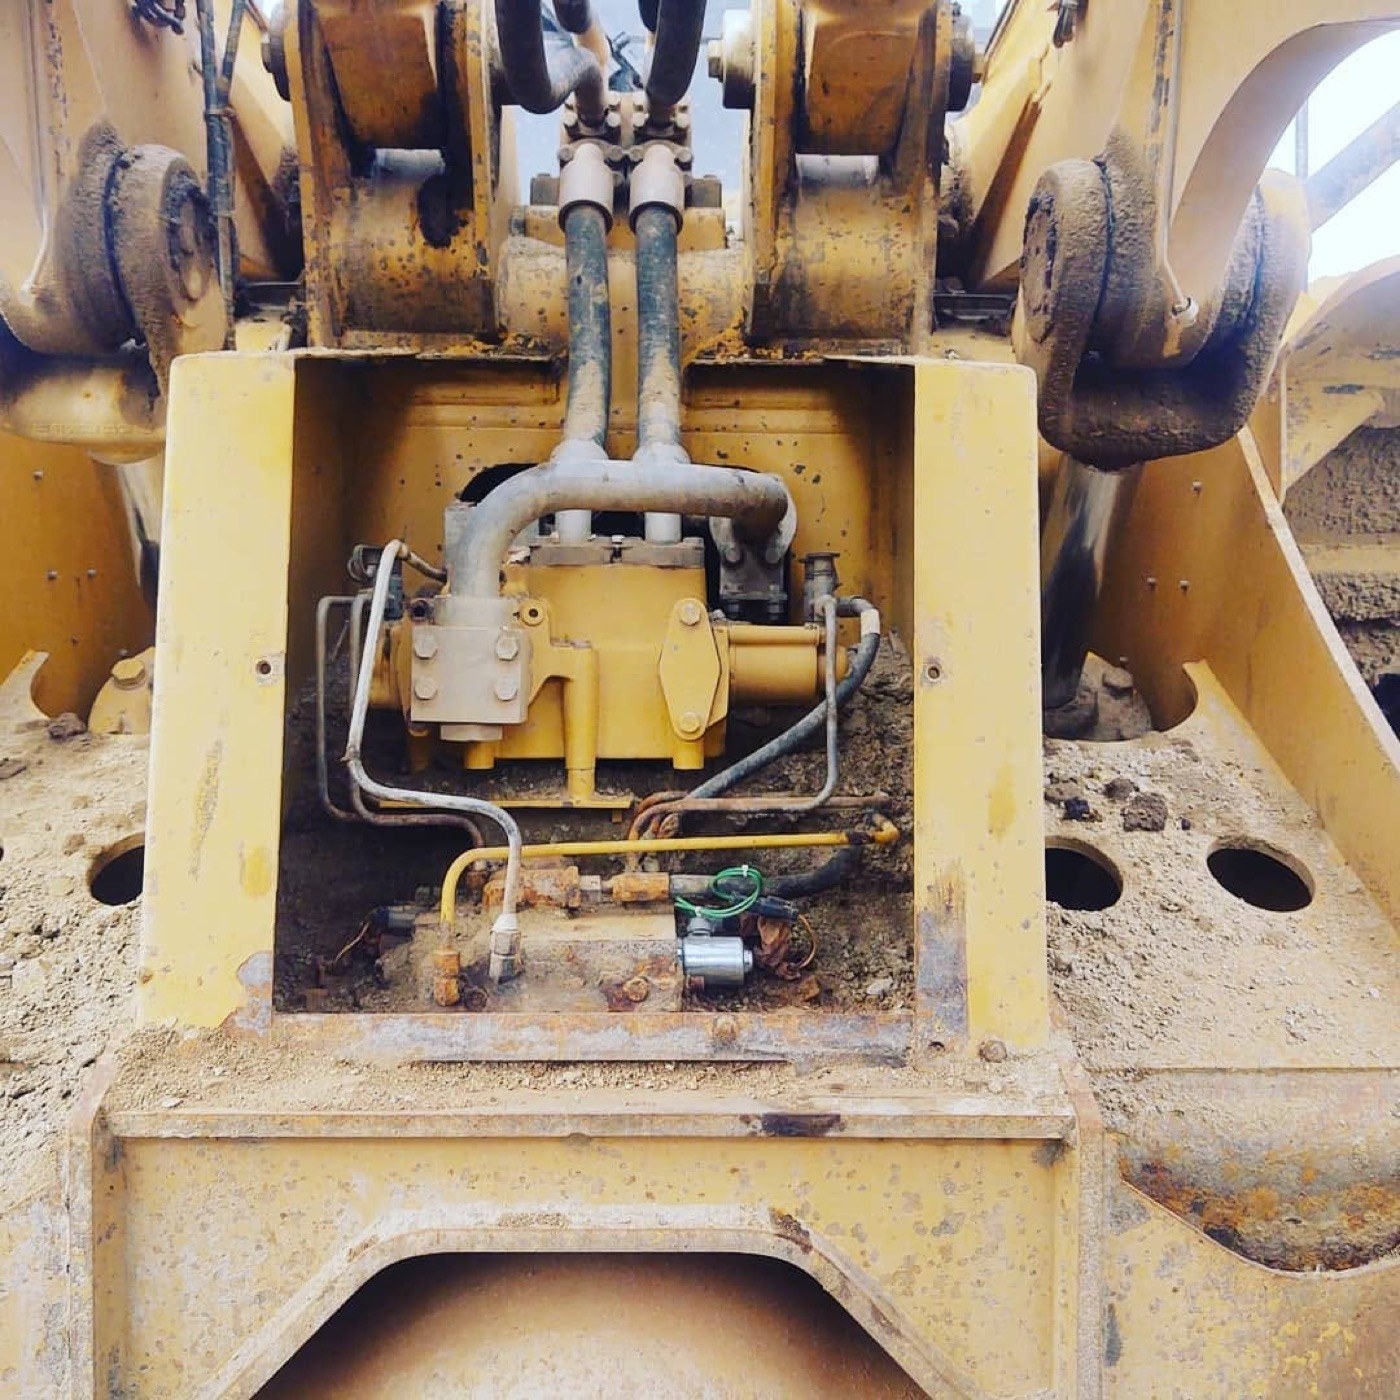 Hydraulic servicesWe repair leaking, slow, and erratic hydraulic systems where the machine is working and rebuild worn hydraulic cylinders.